
10, the bar density is too small cause: a, the temperature is too high; b, screw pressure is small. Heating temperature is too high or too low, forming sleeve wear serious, thruster angle does not match, raw material moisture is too large.
Rod density is too small solution: a, lower the temperature; b, reduce the thread lift angle, increase the screw pressure.
11, the center of the rod density is small, or contains scattered sawdust cause: the thruster shaft tip root diameter of the wear, to fill welding thickening. Shaft tip is not correct will also lead to the above problems, need to be corrected at high temperature.
12, anti-gas: manifested in the production from the lower material mouth outward gas, mainly due to insufficient material supply. May also be due to excessive moisture of raw materials, heating temperature is not enough, etc.
13, "bored car": raw materials mixed with large and hard particles of impurities. Low voltage or heating temperature is low, may also be raw materials are not dry, the former need to stop demolition, remove impurities. The latter to continue to soften the raw materials by heating, or re-drying.
14, rod making machine release the cause: a, the material is too damp; b, rod dead eyes. Improper temperature control, raw material moisture is too large, thruster wear, shaft tip is not correct, the exhaust hole blockage, thruster head spiral is too large or too small, sleeve wear serious, etc.. When encountering this situation, we should check each of the above reasons and make adjustments accordingly after finding out the causes.
The solution of bar making machine discharge: a, adjust the drying temperature, drying the material; b, see the bar dead eye solution. 15, the cause of rod bending: uneven heating, raw material moisture is too large.
Rod bending solution: increase the temperature.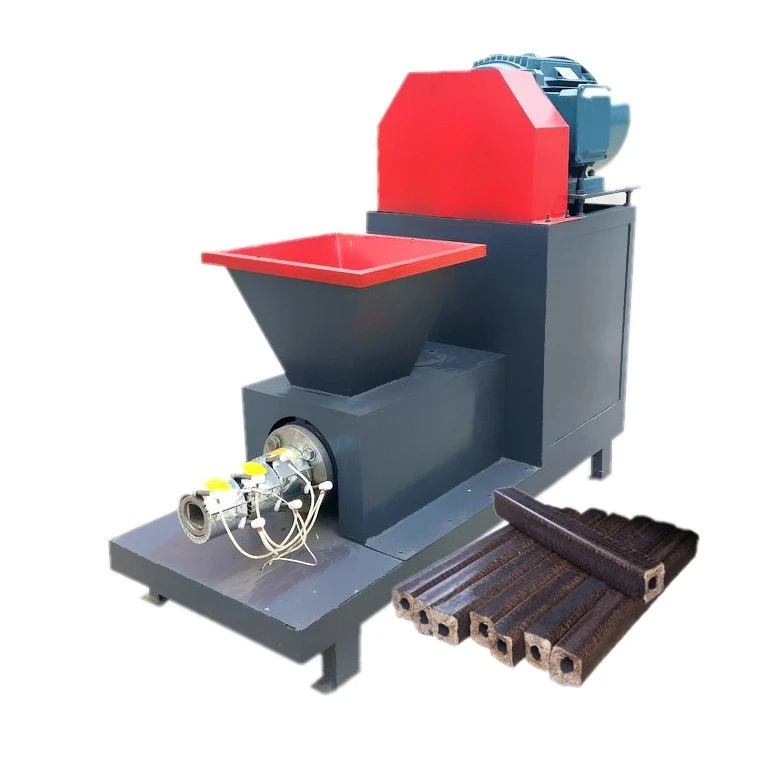
Common faults and solutions of charcoal machine
Nov 22, 2022
Send Inquiry